Shop-Controlled Precision Steelwork Built for Heavy Industrial Duty
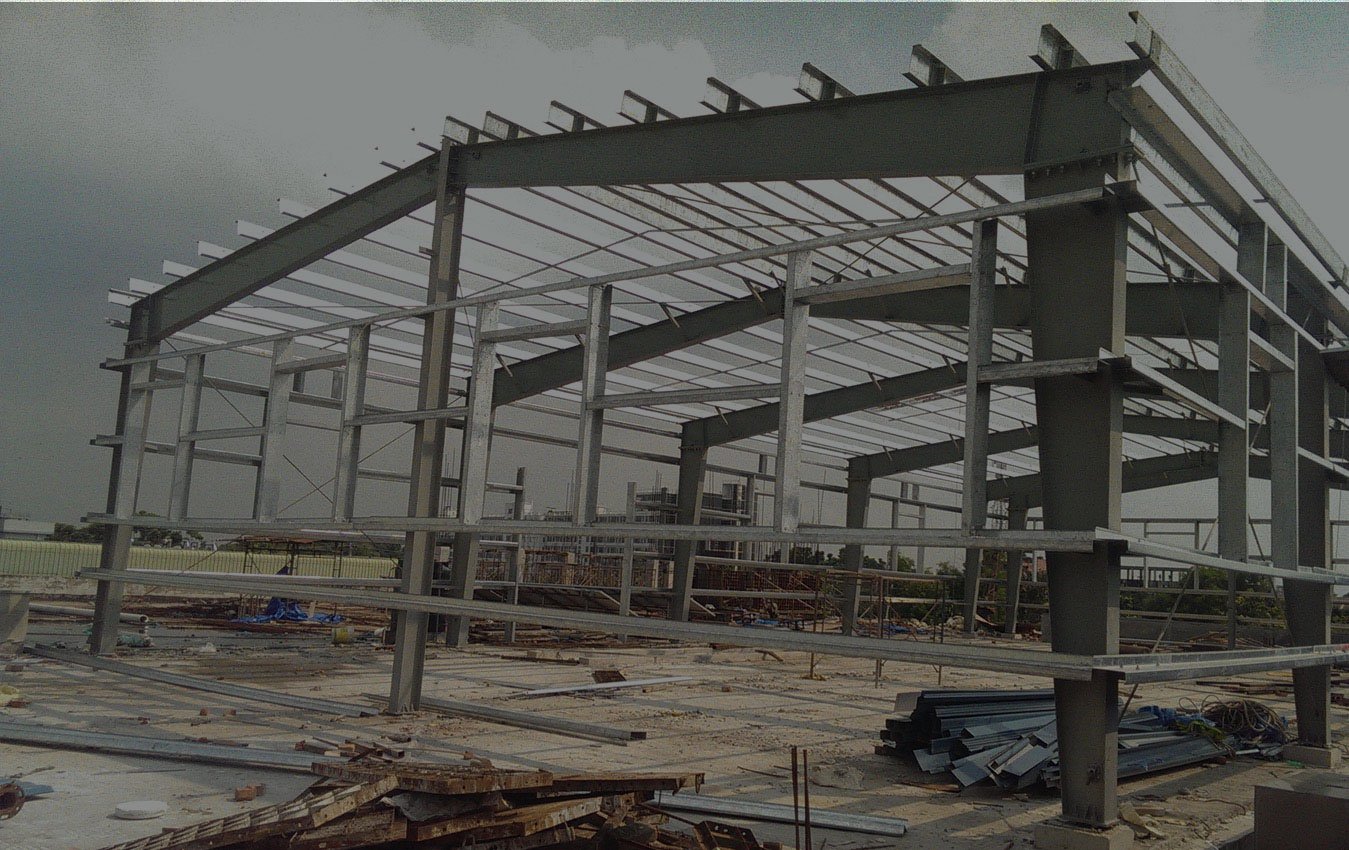
The structural steel-framed building derives its fundamental economic advantage from prefabricated modular components assembled rapidly at site. Unlike in-situ wet concreting, our steel structures are engineered and fabricated within the strictly controlled environment of our Malakhera workshop.
Fabrication carried out in our specialized shop is strictly calibrated and monitored for dimensional accuracy, joint weld penetration, and camber tolerance. On-site field erection is executed by certified riggers using heavy mobile cranes, high-strength friction grip (HSFG) bolts, and laser-guided alignment tools.
Having fabricated over 10,000+ Metric Tonnes of structural steel since 1980 for clients such as Welspun (2,500+ MT), Hero MotoCorp (1,700 MT), and Maruti Suzuki (900 MT), KEW guarantees structural resilience, zero field modifications, and rapid commissioning.
Key Structural Steel Fabrication Assemblies
Custom engineered components built to withstand extreme dynamic, seismic, and mechanical loadings.
Crane Gantries & Runway Beams
Engineered gantry girders supporting up to 50 MT overhead traveling cranes (EOT). Fabricated with precision rail surge stiffeners, calibrated rail clamps, and tight deflection tolerances (L/1000).
High-Span PEB Factory Sheds
Pre-Engineered Building (PEB) systems with clear spans up to 60+ meters without intermediate columns. Complete with cold-formed Z & C purlins, roof ventilators, and coated color profile sheeting.
Industrial Chimneys & Process Stacks
Self-supporting and guyed industrial steel chimneys reaching heights exceeding 120 feet. Rolled from heavy carbon steel plates with thermal expansion joints, internal refractory lining, and sampling platforms.
Heavy Built-Up Columns & Trusses
Submerged-arc welded (SAW) box columns, star columns, Pratt/Warren trusses, and multi-tier mezzanine floor framing for heavy rolling mills, casting foundries, and warehouse distribution centers.
Technical Specifications & Quality Codes
Every fabrication operation follows prescribed Bureau of Indian Standards (BIS) and international codes.
| Parameter | Standard Applied | KEW Verification & Tolerances |
|---|---|---|
| Raw Material Structural Steel | IS 2062 Grade E250 / E350 (SAIL, Tata, Jindal) | 100% Mill Test Certificate (MTC) verified with chemical & tensile test checks |
| Structural Design & Loading | IS 800:2007 (Limit State Method), IS 875 (Wind/Seismic) | STAAD.Pro / Tekla 3D structural analysis for deflection and wind gust loads |
| Welding Procedures & Welders | AWS D1.1 / IS 9595 (WPS & PQR Qualified) | Certified 6G welders; Submerged Arc (SAW) & CO2 MIG continuous welds |
| Non-Destructive Testing (NDT) | IS 4260 / ASME Section V (UT & DPT) | Ultrasonic testing on 100% of butt welds; Dye-penetrant on fillets |
| Surface Preparation | ISO 8501-1 / SSPC-SP 10 (Near-White Blast) | Grit blasting to SA 2.5 profile (40–60 micron anchor pattern) |
| Protective Paint System | ISO 12944 (C3 to C5 Industrial Marine) | Zinc Phosphate Primer (75μm) + Epoxy intermediate + PU finish coat (Total DFT 150-200μm) |
Welspun India Pvt. Ltd. (Anjar, Gujarat)
Challenge: Fabricate, transport, and erect over 2,500 Metric Tonnes of heavy structural trusses, crane gantry runways, and high-bay building frameworks within an aggressive continuous-production industrial zone.
Execution: KEW established dedicated multi-shift fabrication lines at our Alwar yard, transported oversized modular truss segments via heavy hydraulic multi-axle trailers, and deployed tandem hydraulic crane lifts for high-altitude pin-point alignment.
Result: Zero on-site recordable safety incidents, 100% UT weld pass rate on first inspection, and commissioning handed over ahead of scheduled plant trial run.
View Complete Project PortfolioFrequently Asked Questions: Structural Steel Fabrication
Why is off-site shop fabrication preferred over on-site steel fabrication?
Shop fabrication in our Malakhera workshop occurs in a controlled environment protected from ambient weather. We utilize automated submerged-arc welding, rigid jigging for camber control, and mechanized grit blasting. Field fabrication is subject to weather disruptions, poor fit-ups, and inferior paint adherence.
What crane gantry capacity can Krishna Engineering Works engineer?
KEW has successfully fabricated and aligned heavy-duty crane gantry runway systems supporting up to 50 Metric Tonnes overhead cranes for clients like Minaksia Color Coated and Maruti Suzuki. We guarantee surge brace rigidity and rail level tolerance within 2mm.
What quality inspection documentation is provided upon project handover?
Clients receive a comprehensive Quality Dossier including Raw Material Mill Test Certificates (MTC), Ultrasonic (UT) and DPT weld reports, Dry Film Thickness (DFT) paint reports, bolt torque tension records, and as-built drawings.